Comprehensive supply chain capabilities covering helmets, personal protective equipment, training infrastructure, and heavy-duty team luggage tailored for North American sports buyers.
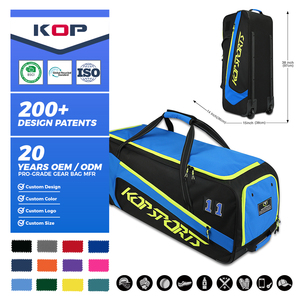
Commercial-grade 1680D nylon construction with padded helmet compartments, side bat sleeves, and heavy-duty off-road tractor wheels for team transport.
Send an Inquiry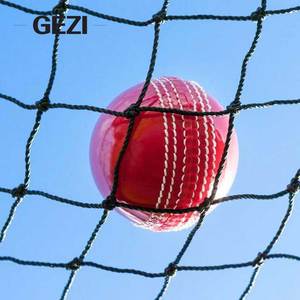
UV-stabilized high-density polyethylene netting designed for indoor commercial facilities and outdoor academy batting tunnels across US climates.
Send an Inquiry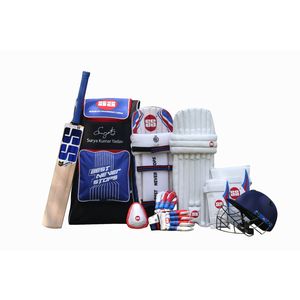
Complete youth safety package featuring Kashmir Willow bat, high-density foam leg guards, protective gloves, and lightweight molded helmet.
Send an Inquiry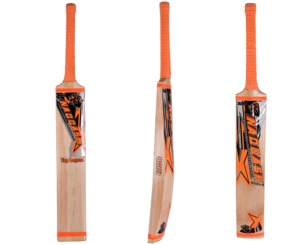
Hand-crafted air-dried willow with thick edges and toe guard protection, balanced specifically for hard leather ball match play in US adult leagues.
Send an Inquiry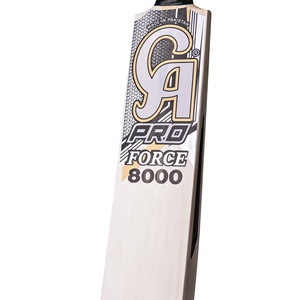
Engineered lightweight wooden blade with exaggerated sweet spot optimized for heavy tape-ball tournaments popular in Texas and California leagues.
Send an Inquiry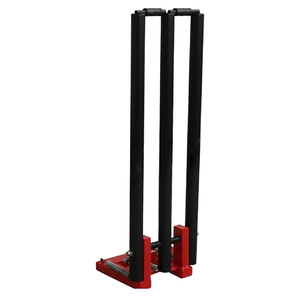
Precision-turned hard ash wood stumps paired with weather-resistant high-impact bails designed for synthetic turf and concrete pitches.
Send an Inquiry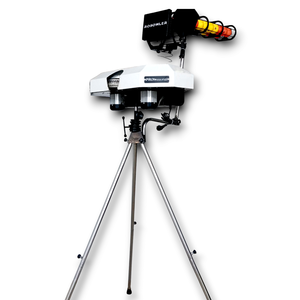
High-precision dual-concave polyurethane wheel system capable of delivering seam, swing, and spin up to 87 mph (140 km/h) for commercial training setups.
Send an Inquiry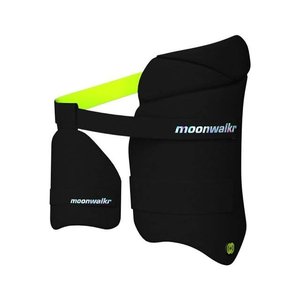
Ultra-lightweight 3D molded composite shell providing anatomical inner and outer thigh protection without restricting running biomechanics.
Send an InquiryAnalyzing localized growth drivers, safety compliance mandates, and procurement trends for US sports equipment distributors and regional league directors.
The establishment of Major League Cricket (MLC), backed by substantial infrastructure investments across Texas (Grand Prairie Stadium), California, North Carolina, and Florida, has fundamentally transformed the demand landscape for cricket equipment in North America. Beyond professional franchises, over 300 youth academies and regional leagues have emerged under the USA Cricket ecosystem. This surge requires bulk procurement of standardized, safety-compliant protective gear, specifically high-impact protective cricket helmets engineered to withstand leather ball velocities exceeding 85 mph.
Unlike recreational sports gear, cricket helmets supplied to the United States market face strict product liability standards and institutional safety guidelines set by scholastic sports boards and regional associations. Modern procurement officers reject generic uncertified headgear in favor of factories capable of providing third-party batch testing documentation under BS 7928:2013 (British Standard for Head Protectors for Cricketers) and alignment with ASTM F1446 impact attenuation protocols. Chinese OEM manufacturing hubs equipped with automated injection molding and precision drop-test towers offer the ideal balance of certified protection and scalable unit economics.
Technical breakdown of energy attenuation liners, composite shell metallurgy, and facial defense architectures manufactured in our advanced production facilities.
Our factory utilizes high-impact engineered ABS (Acrylonitrile Butadiene Styrene) blended with Polycarbonate matrix materials. This combination delivers exceptional flexural modulus and puncture resistance while preventing structural cracking when impacted by 156g hard leather cricket balls at velocities up to 140 km/h.
The core shock-absorption layer features dual-density Expanded Polystyrene (EPS) and Expanded Polypropylene (EPP) liners molded at precise 55g/L density tolerances. This micro-cellular architecture compresses progressively under blunt impact, dissipating peak G-force kinetic energy away from the cranium.
Faceguards are fabricated from high-tensile stainless steel wire or ultra-lightweight Grade-5 Titanium Alloy. Precision laser welding prevents joint shearing during ball impact, while structural geometry guarantees zero ball penetration between the peak and grille gap under BS 7928 testing.
| Component Part | Material Specification | Impact Protection Rating | US B2B Customization Options |
|---|---|---|---|
| Outer Shell | High-Impact Injection Molded ABS / Carbon Hybrid | Resists up to 160 Joules linear kinetic force | Custom PMS Shell Colors, Gloss/Matt Finish, Brand Logos |
| Impact Core | High-Density EPS (55g/L) + EPP Memory Foam Pads | Peak Acceleration < 250G under BS 7928 drop test | Removable Anti-Bacterial Washable Lining, Size Fit Inserts |
| Face Guard (Grille) | High-Tensile Steel Wire / Grade-5 Titanium Alloy | Zero deformation under 140 km/h ball impact test | Powder-Coated Colors, Adjustable Ear-Pads, Quick Release |
| Retention System | Nylon Webbing Strap with Quick-Release Buckle & Chin Cup | Dynamic Roll-Off Resistance > 300N Tension Force | Custom Woven Branding Straps, Molded TPU Chin Guards |
| Ventilation System | Multi-Channel Internal Airflow Ports with Mesh Guards | Engineered thermal comfort for high heat climates | Custom Grille Vent Rings, Dust-Filter Mesh Inserts |
Customizing protective equipment standards for distinct environmental conditions, facilities, and play formats prevalent in the US region.
Indoor sports arenas across cold-weather states (such as New Jersey, New York, Illinois, and Washington) operate high-velocity bowling machines in enclosed cage setups year-round. These facilities demand ultra-durable helmets with high-frequency impact resilience, quick-adjust dial-fit retention systems for rapid player turnarounds, and washable microbial liners that maintain hygiene across multi-user rental programs.
Cricket leagues in Sunbelt regions face intense thermal conditions on concrete and artificial turf grounds. Traditional heavy headgear often leads to heat exhaustion and player fatigue. Our specialized OEM helmet export models incorporate integrated multi-vent heat dissipate channels, moisture-wicking cool-mesh interior padding, and UV-reflective shell finishes specifically engineered for American summer tournaments.
Combining world-class tooling precision, stringent quality assurance, and end-to-end private label support for North American sports equipment importers.
We own and operate state-of-the-art multi-cavity injection molds, high-precision CNC toolrooms, and automatic steel-wire forming machinery. We provide 3D CAD modeling and rapid physical prototyping within 7 to 10 business days for US brands seeking proprietary shell designs or exclusive facial grille profiles.
Quality assurance is embedded into every assembly phase. Incoming ABS resin pellets and steel wires are tested for tensile strength and density. Every finished batch undergoes dynamic drop tests and visor torque testing using AQL 2.5 Sampling Protocol before export documentation and custom master-carton sealing.
Our export desk manages ocean freight (LCL/FCL) directly to major US ports including Los Angeles/Long Beach, New York/New Jersey, and Houston. We provide full retail packaging solutions complete with UPC/EAN barcodes, inner display boxes, and compliance labeling ready for immediate distribution or FBA placement.
Direct technical and commercial answers addressing common inquiries from sports gear buyers in North America.
Yes. All cricket helmets manufactured for our US export partners undergo rigorous third-party laboratory testing to comply with BS 7928:2013 standards, covering both senior (156g) and junior (4.75oz) projectile impact protocols. Furthermore, materials used meet US Consumer Product Safety Commission (CPSC) non-toxic resin and lead-free coating requirements.
Our standard Minimum Order Quantity (MOQ) for custom-branded OEM helmets is 200 to 500 units per colorway/model depending on customization complexity. Pre-production samples are completed within 7 to 14 business days. Upon sample sign-off, bulk production lead times range from 25 to 40 days, coordinated to meet your seasonal stocking deadlines.
Absoltely. We offer comprehensive shell sizing options ranging from Extra Small (Youth 51-53cm), Small (54-56cm), Medium (57-58cm), Large (59-60cm), to Extra Large (Senior 61-62cm). We also manufacture adjustable micro-dial fitment systems integrated into the rear EPS liner to allow one helmet model to comfortably span multiple size ranges.
Cricket helmets are typically classified under HS Code 6506.10.6075 (Safety Headgear / Sports Helmets). Our experienced export logistics team provides all necessary commercial invoices, packing lists, certificate of origin documents, and US Customs entry documentation to ensure smooth port customs clearance.
We follow strict AQL 2.5 Level II inspection guidelines. Before any shipment is approved for container loading, our certified QC inspectors verify structural integrity, shell finish, logo application accuracy, strap tension, and carton labeling. A comprehensive digital inspection report complete with photos and test videos is sent to the client prior to final dispatch.
Yes. We specialize in mixed-product container consolidation for wholesalers and brand owners. You can freely combine certified cricket helmets, Kashmir/English Willow bats, batting pads, wicket keeping gloves, and heavy-duty rolling equipment bags within a single 20ft or 40ft High Cube container, optimizing landed freight costs per unit.
Elevate your brand's protective gear line with BS 7928 certified engineering, factory-direct wholesale pricing, and dedicated OEM support for the North American market.