Direct-from-factory wholesale offerings optimized for global distributors, professional clubs, and sports apparel retailers. Every batch strictly tested to meet international AQL 2.5 quality parameters.
In the rapidly evolving global marketplace, international procurement directors, sports retail chains, and athletic brand managers are re-evaluating their wholesale sourcing frameworks. Choosing a reliable China wholesale sports apparel supplier and exporter requires an operational understanding that extends beyond unit price. Modern procurement strategies prioritize structural material integrity, supply chain transparency, strict compliance with environmental protocols (such as REACH and OEKO-TEX Standard 100), and rapid prototyping capabilities.
As global consumer demand shifts toward multi-functional activewear, high-performance teamwear, and specialized protective sports equipment, suppliers must provide demonstrable Information Gain. This report analyzes the operational benchmarks, materials technology, quality assurance frameworks, and future market trajectories defining the international sports goods trade.
Our manufacturing facilities integrate specialized craftsmanship with automated production technologies, ensuring high consistency from preliminary sample approval to bulk container delivery.
We operate strictly on client tech-packs and precise engineering parameters. From specialized GSM fabric weights and custom pantone matching to bespoke ergonomic padding curves in protective gear, our OEM team turns technical specifications into production-ready output.
Quality control is built into every step. We conduct raw material incoming verification, in-line process checks during stitching or molding, and final randomized box sampling under AQL 2.5 standards prior to export clearance.
Serving over 17 countries across North America, Europe, Oceania, and Asia, our logistics department manages complex customs documentation, palletization, barcode compliance, and flexible shipping terms (FOB, CIF, DDP).
Understanding where the athletic equipment and sports wear market is heading allows wholesale buyers to future-proof their supply chains and gain market share.
Environmental compliance has transitioned from a marketing point to a mandatory procurement requirement. Global buyers are actively shifting away from virgin petroleum-based synthetics. Future procurement standardizes rPET (Recycled Polyethylene Terephthalate) derived from ocean plastics, organic cotton blends, and waterless sublimation printing dyes that dramatically reduce chemical effluent. In hardware manufacturing, eco-friendly polyurethane (PU) and bio-based resin compounds are replacing traditional PVC coatings.
Next-generation athletic apparel demands intelligent micro-ventilation and zone-mapped compression features. High-density moisture-wicking fabrics engineered with micro-channel cross-section yarns allow rapid evaporative cooling during high-intensity performance. Advanced flat-lock stitching and seamless bonding prevent friction points, extending garment durability under rigorous match conditions.
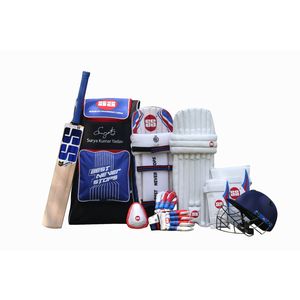
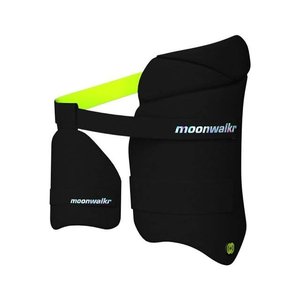
In protective sports equipment—such as cricket pads, thigh guards, and combat equipment—the shift toward ultra-lightweight multi-density EVA foams and dynamic shock-absorbing TPU shells is paramount. Modern protective wear must deliver ergonomic mobility without compromising impact dissipation energy metrics. Digital 3D scanning and computer-aided molding are becoming standard in custom OEM protective production.
Lead time reduction is the primary focus for competitive sportswear retailers. Through digital 3D garment rendering and automated pattern cutting, pre-production sample approval timelines have decreased from weeks to days. Automated stitching machinery and laser-guided cutting ensure dimensional accuracy across high-volume production runs.
Comparative evaluation matrix for B2B sports goods buyers planning wholesale volume orders.
| Product Division | Core Material Grades | Customization Capabilities | Standard Lead Time | Quality Testing Protocols |
|---|---|---|---|---|
| Custom Teamwear & Apparel | Recycled Polyester, Micro-Mesh, Spandex (140-280 GSM) | Full Sublimation, Heat Transfer, Screen Print, Custom Sizing | 20 - 30 Days | Color Fastness, Abrasion Resistance, Tensile Strength |
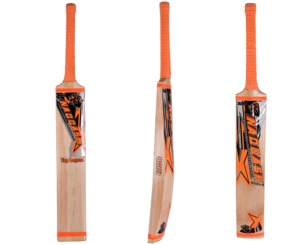
| Cricket Equipment & Bats | Kashmir Willow, Premium English Willow, Compressed Cane | Custom Weight Balancing, Handle Rubber Grips, Branding Sheets | 25 - 40 Days | Moisture Content Analysis, Impact Resilience, Grain Inspection |
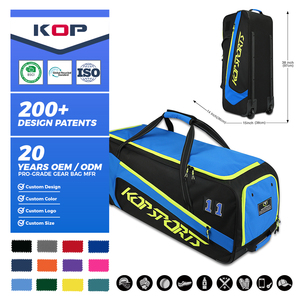
| Sports Bags & Luggage | 600D/1680D Heavy Duty Nylon, Waterproof TPU, Reinforced Canvas | Heavy-Duty Wheel Chassis, Custom Dividers, Embroidered Logos | 30 - 45 Days | Zip Endurance Testing, Strap Load Strength, Water Resistance |
| Protective Guards & Pads | High-Density EVA Foam, Polycarbonate Shells, Breathable PU Cover | Ergonomic Dynamic Fit, Dual Strap Systems, Custom Colorways | 25 - 35 Days | Impact Force Absorption, Stitch Tensile Test, Flex Life Test |
Clear, transparent answers regarding enterprise OEM contracts, manufacturing capabilities, and export procedures.
Partner with an established manufacturer committed to precision engineering, reliable delivery schedules, and competitive factory-direct pricing. Request our complete wholesale catalog and schedule a technical consultation with our engineering team today.