High-performance athletic teamwear manufactured with precision digital dye-sublimation, moisture-wicking synthetic fibers, and tournament-grade durability.
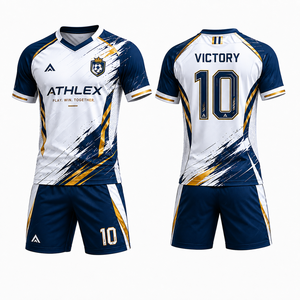
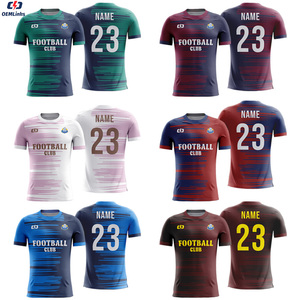
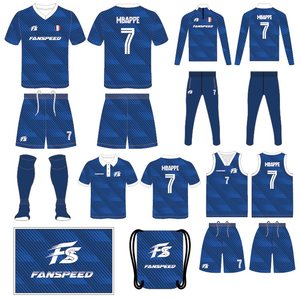
The global sportswear and athletic apparel market is undergoing a seismic paradigm shift. Modern sports organizations, university leagues, professional clubs, and commercial sportswear brands no longer demand simple mass production; they require high-precision customization, rapid-turnaround supply chains, eco-responsible textile formulations, and uncompromised structural durability. As premier China Team Uniforms Suppliers and OEM/ODM Manufacturers, our facility stands at the convergence of advanced textile science, automated digital production, and lean global logistics.
Navigating international teamwear procurement requires deep insights into manufacturing engineering, fabric technology, and quality control systems. China's sportswear manufacturing ecosystem has evolved from legacy cut-and-sew operations into fully integrated digital micro-factories capable of delivering bespoke dye-sublimated garments with zero color variance across multi-thousand unit production runs. This whitepaper provides procurement directors, brand owners, and sports equipment distributors with the comprehensive technical knowledge required to optimize their teamwear supply chain, mitigate quality risks, and secure superior information gain in product engineering.
To maintain competitive advantage in global wholesale apparel procurement, buyers must understand the core technological shifts driving modern uniform manufacturing:
Utilizing high-density Swiss and Italian eco-friendly sublimated inks to ensure 100% color fastness, vibrant pantone matching, and zero fabric pore blockage.
Computerized laser cutting tables ensure pattern piece precision down to 0.1mm, preventing seam distortion and guaranteeing perfect anatomical fit across size sets.
Rigorous three-stage quality control adhering to ISO 9001 and AQL 2.5 standards: raw fabric verification, in-line process checks, and pre-shipment inspections.
At the core of every premium athletic uniform lies polymer science and yarn construction. Modern sports apparel must balance contradictory physical requirements: high tensile strength vs. ultra-lightweight breathability, elastic stretch recovery vs. dimensional stability under friction. Our factory utilizes engineered synthetic knits specifically tailored to the physiological demands of each sport discipline.
Standard polyester fabrics trap body heat and moisture, leading to athlete fatigue and thermal discomfort. Our professional soccer, basketball, and running uniforms utilize cross-section micro-filament yarns (such as CoolMax and Dri-FIT mesh structures). These fibers create microscopic channels that pull liquid sweat away from the epidermis via capillary action, spreading it across an expanded outer surface area for rapid evaporation within seconds.
In response to global ESG (Environmental, Social, and Governance) mandates, our factory has introduced GRS (Global Recycled Standard) certified RPET performance yarns. Derived from post-consumer recycled plastic bottles, our eco-friendly fabrics reduce carbon emissions by up to 45% and energy consumption by 52% compared to virgin polyester, without sacrificing tensile strength, soft hand-feel, or color brilliance.
| Sport Category | Recommended Fabric Composition | Fabric Weight (GSM) | Stitching Construction | Key Performance Attribute |
|---|---|---|---|---|
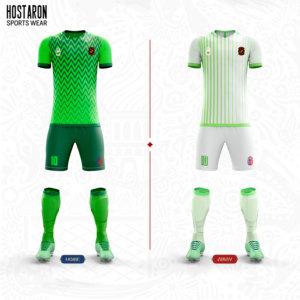
| Professional Soccer Kits | 100% Interlock / Birdseye Mesh Polyester | 140 - 160 GSM | Reinforced Flatlock / Double-Needle | Ultra-lightweight, rapid dry, moisture transport |
| Basketball Uniforms | 100% Heavyweight Pin-Hole Mesh / Shiny Tricot | 180 - 220 GSM | Heavy-duty cover-stitching | Maximum air circulation, abrasion resistance |
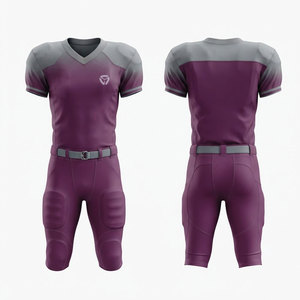
| American Football / Rugby | 92% Polyester + 8% Spandex Heavy Dazzle | 260 - 320 GSM | 4-Needle 6-Thread Reinforced Seams | Extreme tear strength, 4-way stretch elasticity |
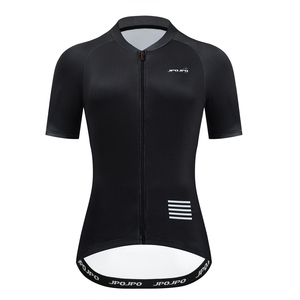
| Aerodynamic Cycling Apparel | 80% Nylon / Polyester + 20% Elastane Mesh | 130 - 180 GSM | Anatomical Flat-seam Ergonomic Cut | Aerodynamic drag reduction, muscle compression |
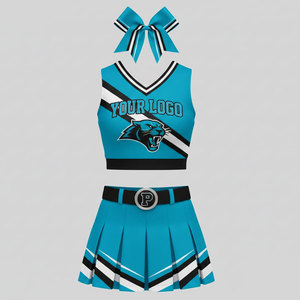
| Cheerleading & Gymnastics | 85% Polyester + 15% High-Gloss Spandex | 200 - 250 GSM | Seamless high-flex stretch binding | Full 360-degree range of motion, foil durability |
To eliminate procurement friction for global distributors, our China factory employs a transparent 4-stage OEM/ODM operational workflow. This structured engineering approach guarantees that every bulk shipment aligns precisely with approved pre-production golden samples.
Our design engineers review client AI/PDF artwork files, map Pantone TCX/C colors, verify sizing spec charts, and optimize graphic scaling across XS to 5XL sizes.
We create a complete physical sample incorporating full sublimation, custom neck labels, woven side badges, silicone chest logos, and retail hangtags for client sign-off.
Upon sample approval, high-speed digital printers (Mimaki & Epson) run 24/7 alongside automated fabric spreaders and laser cutters, ensuring continuous output.
During Stage 3, in-line quality assurance technicians perform tension testing on seams, color-bleed evaluation under ISO 105 standards, and barcode scanning on individual retail polybags. This rigorous operational discipline has established our factory as a trusted export partner across 17+ countries, including the USA, UK, Australia, Germany, and Canada.
As we look toward the 2026-2030 sourcing cycles, several emerging macro trends are reshaping how sports equipment distributors and club gear managers select their Chinese manufacturing partners:
Legacy supply chains required massive minimum orders (1,000+ units per style), resulting in excessive inventory risk and bloated storage costs. Modern digital sublimation technology enables flexible micro-batch manufacturing. Our plant comfortably handles low-MOQ orders (starting at just 10-50 units per design for club re-orders) while maintaining wholesale factory pricing.
Next-generation athletic apparel is evolving to accommodate biometric sensors, GPS tracking units, and telemetry devices. Our R&D team is actively engineering integrated mesh pockets, internal conductive fabric channels, and reinforced sensor mounts within professional American football, soccer, and rugby jerseys for elite club tracking systems.
Post-exercise bacterial growth is a major cause of fabric degradation and unpleasant odors in synthetic teamwear. Our uniforms undergo silver-ion (Ag+) and zinc-based antimicrobial finishing treatments. This surface coating inhibits bacterial cell wall synthesis, maintaining garment freshness through 50+ industrial wash cycles.
Critical operational insights addressed directly by our senior technical director and export logistics managers.
With over two decades of dedicated manufacturing experience in high-performance sports equipment and custom athletic apparel, our organization represents the benchmark of reliability, technical expertise, and customer-centric service. We have successfully supplied over 500+ global brands, school districts, professional leagues, and regional distributors across 17+ countries.
Every individual garment undergoes manual seam-stress verification, measurement auditing against specs, thread trimming, and stain checking before entering the packing line.
By eliminating middleman brokers and optimizing fabric yields through computerized nesting software, we pass 15-30% cost savings directly to our brand partners.
Your account is managed by a bilingual apparel engineer who understands fabric GSM, seam allowances, and vector graphics, ensuring flawless technical communication.
Contact our export engineering desk today to request a free tech pack consultation, fabric sample kit, or instant factory quotation. We reply within 8 hours.
Send an Inquiry