Custom sublimated apparel built with advanced moisture-wicking synthetic fabrics, high-density stitching, and fully customizable club branding.
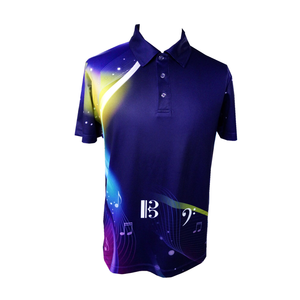
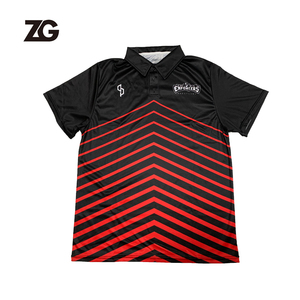
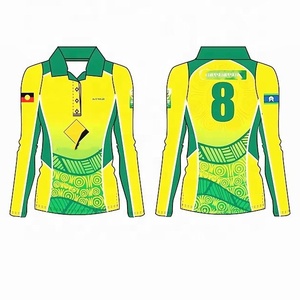
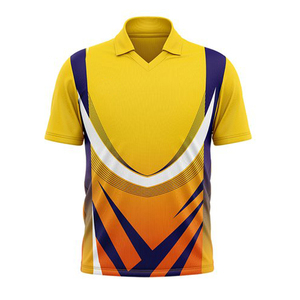
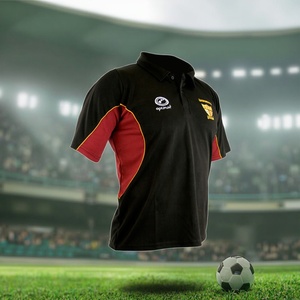
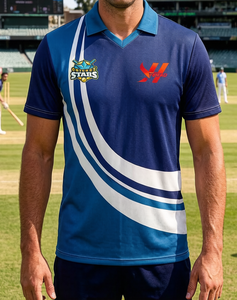
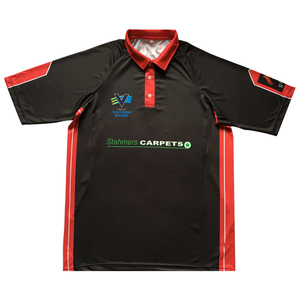
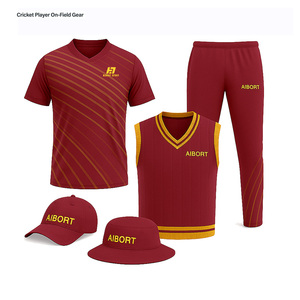
Cricket sportswear has transitioned from traditional heavy cotton knits to modern, scientifically formulated polymer textiles. As a premier China Top Cricket Wear Supplier & Exporter, our manufacturing architecture integrates advanced thermal dynamics, mechanical elasticity, and high-fidelity sublimation technology to meet the extreme physical demands of professional bowlers, batters, and fielders across diverse climatic zones.
Information Gain Metric: Standard off-the-shelf sportswear retains up to 18% of absorbed sweat weight during high-intensity 40°C match conditions. Our proprietary micro-porous 100% polyester weaves restrict moisture retention to under 2.4%, returning optimal thermoregulation back to the athlete within seconds.
High-level cricket performance demands distinct fabric behaviors depending on match formats (T20, One Day Internationals, and Multi-Day Test matches). Our R&D division specializes in four primary fabric compositions designed specifically for custom OEM apparel manufacturing:
Digital sublimation printing represents the gold standard for modern teamwear customization. Cheap screen printing cracks, adds unwanted garment weight, and restricts breathability. We utilize state-of-the-art Japanese Mimaki printer arrays combined with genuine Italian Kian™ sublimation inks. Thermal transfer occurs at precisely 210°C under 5.5 bar pressure, permanently bonding non-toxic dyestuffs into the polyester microfibers at a molecular level.
This process ensures absolute color fastness (Grade 4.5+ under ISO 105-CO6 standards), zero loss of fabric breathability, zero color bleeding under sweat, and microscopic rendering accuracy for complex sponsor logos, gradient patterns, and intricate club crests.
| Performance Class | Fabric Composition | Weight (GSM) | Stitching Construction | Key Applications | Recommended Customization |
|---|---|---|---|---|---|
| Pro League Match Grade | 92% Poly / 8% Spandex | 155 GSM | 4-Needle 6-Thread Flatlock | T20 Franchises / ODIs | Full Sublimation + 3D Silicon Crest |
| Tournament Club Grade | 100% Micro Mesh Polyester | 160 GSM | Reinforced Double-Stitched Hem | Club Leagues & Academies | Sublimation + Screen Print Sponsor |
| Training & Casual Polo | 100% Poly Pique Knit | 180 GSM | Overlocked Seams & Rib Collar | Coaching Staff / Retail Lines | Embroidered Logo + Sublimation |
| High-Mobility Trousers | 100% Heavy Duty Stretch Poly | 210 GSM | Triple-Thread Inseam Seam | Match Whites / Colored Pants | Piping + Zipper Pockets + Sublimation |
As international cricket expands into non-traditional markets—accentuated by cricket’s inclusion in the Los Angeles 2028 Olympic Games—the global procurement landscape for cricket apparel is undergoing a structural shift. Distributors and brand managers must align their supply chains with four decisive market trends:
Global retailers are transitioning to Recycled Polyethylene Terephthalate (rPET) made from ocean-bound plastic bottles. Our eco-line reduces carbon emissions by 45% while retaining identical moisture-wicking and tensile specs.
Traditional 90-day lead times are obsolete. League franchise models demand rapid 7-to-14-day sample turnarounds and 25-day bulk delivery to react quickly to late sponsor signings and team roster announcements.
Overseas buyers now mandate ISO-compliant, documented batch testing. Our zero-defect philosophy uses strict AQL 2.5 sampling standards covering seam strength, color fastness, sizing accuracy, and barcode integrity.
Navigating offshore manufacturing requires a partner with deep domain expertise, scalable infrastructure, and transparent export logistics. Our state-of-the-art facility combines cutting-edge automated cutting machinery with skilled textile artisans to deliver unprecedented quality controls for sports distributors across 50+ countries.
We provide full end-to-end OEM and private-label solutions tailored to international importers, sports apparel brands, and large-scale league organizers:
From classic mandarin collar designs to side-slit breathable athletic cuts, our pattern masters craft bespoke tech packs fitted precisely to Asian, European, or Western sizing tables.
We supply retail-ready hang tags, woven collar labels, polybag packaging with scannable EAN/UPC barcodes, and custom branded master shipping boxes.
Quality control operates in 3 distinct tiers: incoming raw fabric inspection, in-line stitching stress checks, and post-sublimation color calibration tests prior to dispatch.
Clear, definitive answers regarding custom orders, minimum order quantities (MOQs), shipping logistics, and technical customization options.
Our standard MOQ is flexible to accommodate both large distributors and local leagues. For fully customized sublimated jerseys and trousers, our MOQ starts at just 50 pieces per design across mixed sizing sets. For custom fabric dyes or bespoke fabric developments, MOQs start at 300 pieces.
Pre-production sample development typically takes 7 to 10 business days upon digital artwork approval. Bulk manufacturing timelines range between 20 to 35 calendar days depending on total order volume and complexity. Expedited air shipping (5-7 days door-to-door) or sea freight (LCL/FCL) options are managed directly by our export logistics desk.
Yes. We utilize the official Pantone Matching System (PMS) to ensure 100% color accuracy. Our digital sublimation workflow uses high-resolution vector files (.AI, .EPS, or high-res .PDF) to print pin-sharp sponsor logos, club crests, player names, and numbers without extra set-up fees.
All garments follow ISO 9001 quality frameworks and AQL 2.5 final inspection protocols. Measurements are verified against locked pre-production physical tech samples. Tensile strength, color fastness, seam elasticity, and zipper smooth-action tests are conducted before packaging authorization.
Yes. We supply GRS (Global Recycled Standard) certified 100% recycled polyester (rPET) derived from post-consumer plastic bottles. It maintains identical breathability, lightness, and moisture-wicking characteristics as virgin polyester while providing a strong sustainability narrative for modern sportswear brands.
We provide retail-ready private labeling including custom woven collar tags, satin care labels, heat-seal size transfers, custom hang tags, individual branded polybags, and scannable SKU barcode labels on master export cartons for seamless warehouse integration.